When no catalogue insert does the job, custom carbide inserts can be ground to your drawing, usually starting from a standard carbide blank of the nearest shape. We take these orders from a sketch or a dimensioned photo, and you approve a drawing before anything is ground. Below is one such order from first email to delivery, and the list of what we need from you to quote one.
Most turning and grooving work is covered by standard geometries. A special starts to make sense when the part itself dictates the shape: a groove with an undercut or a step, a profile that would otherwise need two tools and two passes, or a holder that sits so close to a shoulder that the standard insert rubs where it should clear. In those cases a small change to a stock insert, a relief angle or a notch, is often all it takes.
Typical modifications are relief and back angles, notches and steps, form profiles, specific corner radii, a sharp or honed edge, and the choice between coated and uncoated carbide.
In May 2026 a customer in Eastern Canada asked whether we could grind custom lathe grooving inserts. The starting point was a sketch and a standard 4 mm top-notch grooving insert, NG4M400RK. They needed two versions of it:
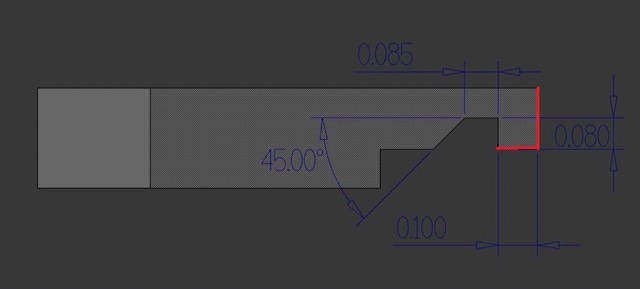
The part is made of 6061 aluminum, and nothing else runs on these inserts.
The customer offered to send their own inserts for modification. We quoted new ones instead: a carbide blank of the same geometry, ground to shape. Shipping original inserts to the grinding shop and back would have added freight and import duty to every piece.
The first request came as two photos with dimensions. Before quoting, the grinding shop asked whether the 15° was a rake angle or a relief that keeps the cutting edge intact, and asked for the workpiece material and hardness to set the edge preparation. We then turned the photos into proper drawings and sent them to the customer for approval. Their corrections:
The drawings were approved in early July. The grinding fixture was made while the blanks were on their way, so grinding started right after approval.
The customer's first request was 7 and 8 pieces. A grinding shop sets up a fixture and a program for each shape, so it runs these in batches: the minimum was 50 pieces per order. The customer split it 30 of 2499F and 20 of 2499R, at the same price per piece as a single model, because the price depends on the blank and the number of setups rather than on how complex each feature is.
A few inserts failed inspection at the grinding shop and were scrapped. We shipped 23 of 2499F and 19 of 2499R in August and invoiced the quantity actually delivered. Five weeks after the drawings were approved, the inserts were on their way from our warehouse to the customer.
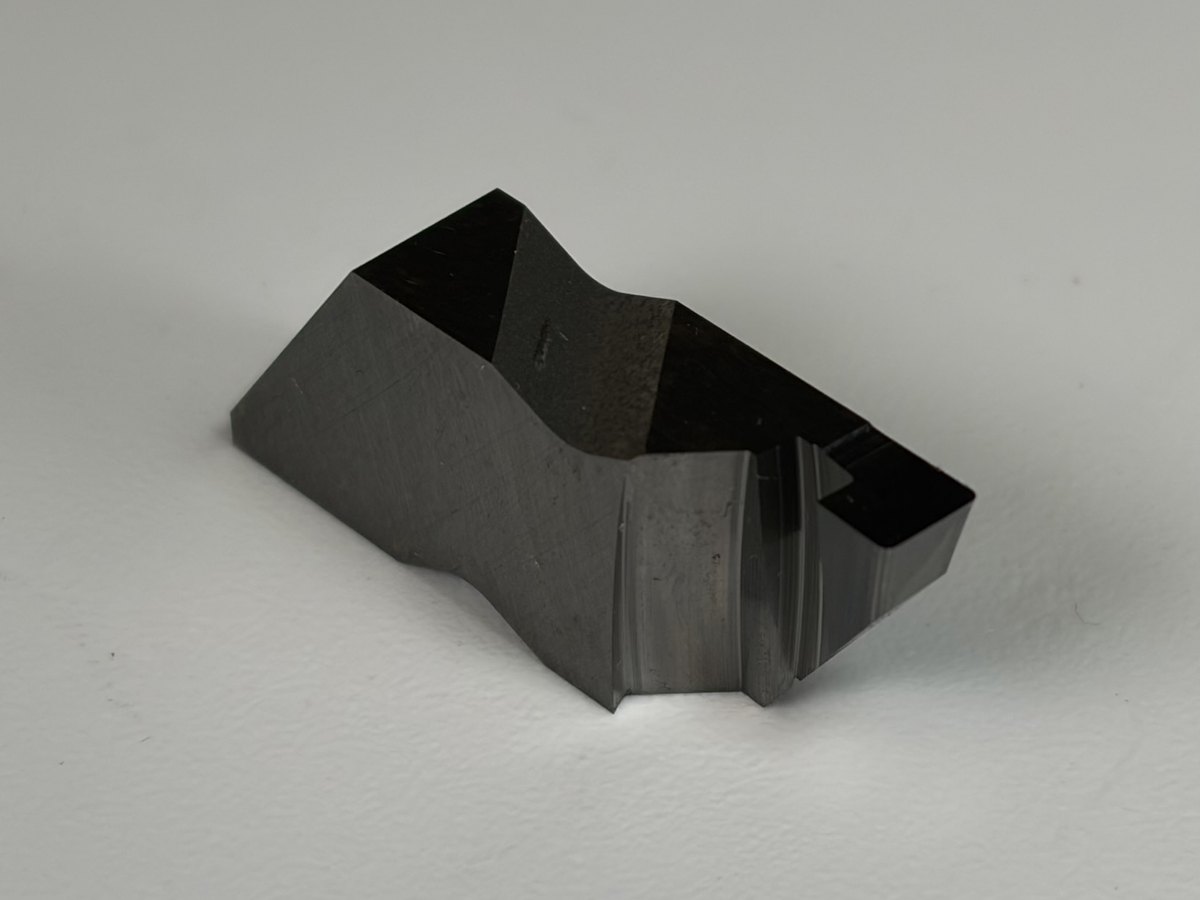
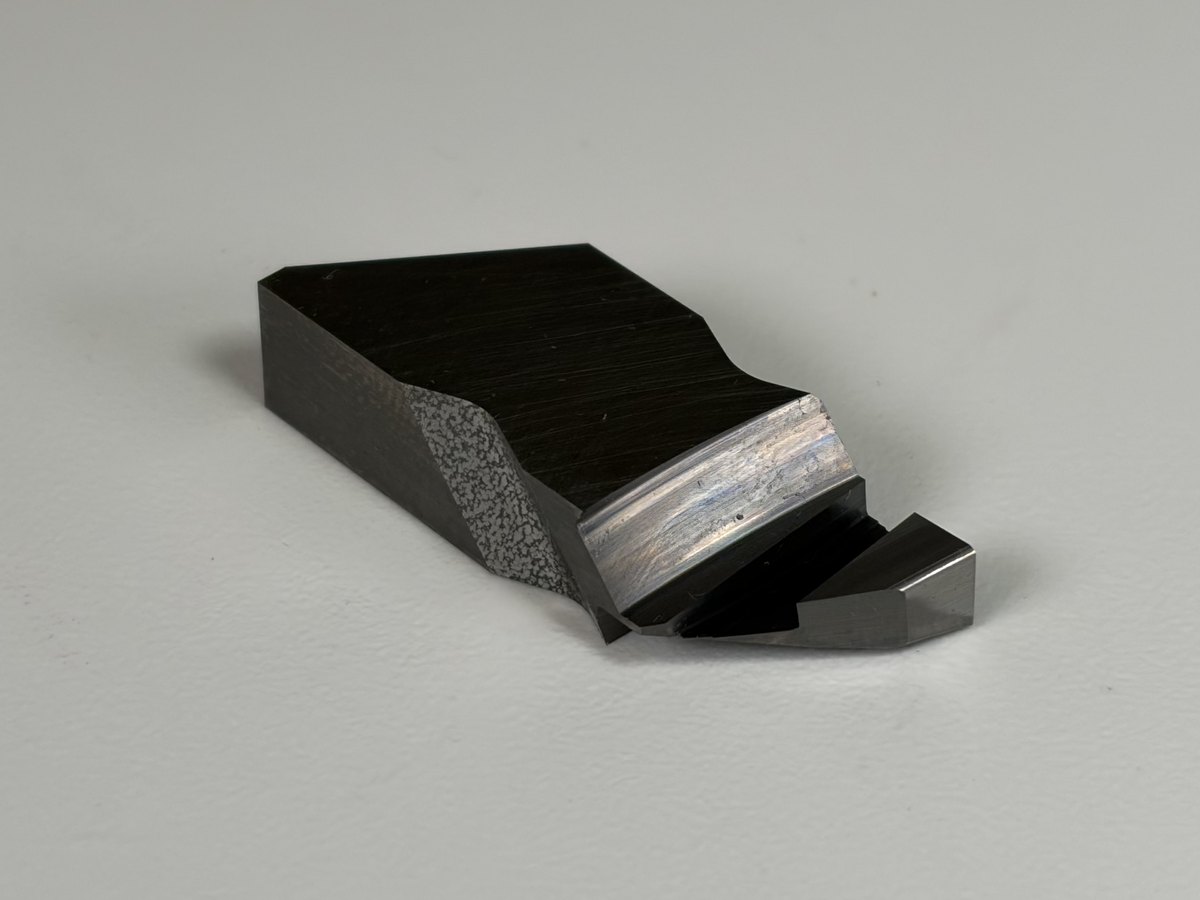
The customer reported that the inserts perform well. They came out slightly shorter than the originals in the holder, which the customer attributed to variation between holders and solved by facing off the end of the holder. The practical lesson: send the holder reference with the drawing and state which length matters.
Send it through the form below. We reply with questions first, then a quote.
